If you’ve ever spent time around heavy industrial machinery—from a paper mill’s rolling presses to a wind turbine’s gearbox—chances are you’ve relied on fluid film bearings without even realizing it. Unlike their rolling-element cousins, these bearings operate on a thin layer of lubricant (oil, grease, or even water) that separates the rotating and stationary parts, eliminating metal-on-metal contact, cutting friction, and extending equipment life. As a fluid film bearing supplier, I get calls every week from maintenance managers, design engineers, and plant operators asking the same question: How do we actually calculate how much weight, force, or load these bearings can handle? It’s not just a number—it’s the difference between a bearing that lasts 5 years and one that fails in 6 months, between unplanned downtime that costs six figures and smooth, consistent production. Fluid Film Bearings
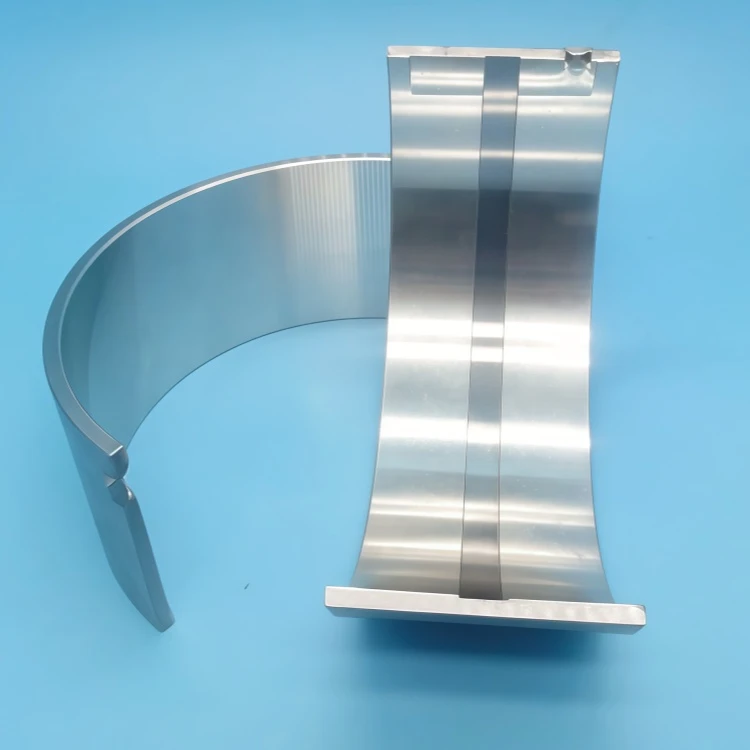
Let me start by cutting through the jargon. Calculating load-carrying capacity for fluid film bearings isn’t about pulling a random formula out of a textbook. It’s about balancing four core factors: lubricant properties, bearing geometry, operating speed, and the environment the bearing will live in. I’ve been in this business for 12 years, and I can tell you that the best calculations I’ve ever done came from walking a customer’s plant floor, not just crunching numbers in an office. That said, there are foundational steps every engineer should follow, and common mistakes I see new suppliers (and even some seasoned ones) make all the time.
First, let’s define what we mean by “load” here. Fluid film bearings handle two main types of loads: radial loads (the force pushing perpendicular to the shaft, like the weight of a gear sitting on a shaft) and thrust loads (the force pushing along the shaft’s axis, like the pressure from a propeller on a marine engine). Some bearings, like our standard radial sleeve bearings, are optimized for radial loads, while thrust bearings (a specialty we manufacture for marine and turbine applications) handle only axial loads. Misidentifying which load type you’re dealing with is the first big mistake. Last year, a steel mill engineer reached out to us because their thrust bearing was failing every 18 months, but they’d ordered a radial bearing by mistake—they just swapped the part without adjusting the load calculation. That’s the kind of error that leads to unnecessary costs, so let’s nail down load type first.
Next, the single most critical factor in load-carrying capacity is the lubricant’s viscosity. Viscosity is just oil’s thickness, right? But it’s not as simple as “thicker is better.” Viscosity decreases as temperature increases—something we call viscosity-temperature (V-T) behavior, a graph every bearing engineer should memorize. The minimum film thickness— the gap between the shaft and bearing that keeps metal apart—depends entirely on how thick the lubricant is at the bearing’s operating temperature. If your bearing runs hot (common in high-speed equipment), your oil will thin out, and if it’s too thin, the film breaks down, leading to wear. The formula here is straightforward, but only if you get the right viscosity value: we use ISO standard viscosity grades, like ISO 32 or ISO 68, and always verify what viscosity the customer’s equipment will hit at full load and full operating temperature, not just the ambient temperature. I can’t tell you how many times I’ve heard a customer say “we use ISO 46 oil” but didn’t account for the fact that at 180°F, that oil’s viscosity drops to 22 cSt—way below what’s needed for a 10,000-lb radial load on a 6-inch bearing.
Then there’s bearing geometry, the shape and size of the bearing itself. For the most common type, cylindrical sleeve bearings, load-carrying capacity scales with two key dimensions: the bearing’s diameter (let’s call that D) and its length (L). The ratio L/D is make-or-break here. A bearing with a higher L/D ratio (like 1.5, meaning the length is 1.5 times the diameter) can handle more load than a short, wide bearing (L/D = 0.5) of the same diameter. Why? Because the load is distributed over a larger contact area between the lubricant and the bearing. But here’s the catch: too high an L/D ratio can lead to alignment issues in the shaft, which causes uneven loading and film breakdown. We always advise customers to match L/D to their application: high-load, slow-speed equipment (like crusher shafts) do well with L/D of 1 to 1.5, while high-speed, low-load equipment (like small motor shafts) works best with L/D of 0.5 to 0.7. For thrust bearings, geometry is different—we use pad bearings, where each pad supports a portion of the load, so the number of pads and their tilt (for hydrostatic bearings) directly impacts capacity. A customer in the wind energy sector came to us last year with a thrust bearing for a 3MW turbine; their initial design used 3 pads, but we recommended 5 pads, which spread the load evenly and increased capacity by 40% without making the bearing any larger.
Speed is another non-negotiable variable. Fluid film bearings operate in two main regimes: hydrodynamic (where the shaft’s rotation pulls lubricant into the gap, creating pressure to support the load) and hydrostatic (where an external pump forces lubricant into the gap, common for very heavy loads or low-speed applications, like ship rudders). For hydrodynamic bearings, load-carrying capacity increases with speed—faster rotation means more lubricant is pumped into the gap, higher pressure, and the film can support more weight. But for hydrostatic bearings, speed plays almost no role, because the pressure comes from the pump, not the shaft’s motion. That’s a key difference I see engineers mix up all the time. For example, a mining conveyor that runs at 5 RPM isn’t going to create enough hydrodynamic pressure on its own, so a hydrostatic bearing with a pump is the right choice. I once had a customer try to use a hydrodynamic bearing on a conveyor that operated at 3 RPM; the bearing seized in 2 weeks, and they had to replace it with our hydrostatic unit at a cost that was actually lower than the downtime they saved. That’s a real-world example of how getting the speed regime right makes all the difference.
Once you have these base variables—load type, lubricant viscosity, L/D ratio, and speed—you can move to the formal calculation, though it’s always wise to get an engineer from a bearing supplier like us to verify it, not just rely on in-house spreadsheets. Let’s walk through a real example, something I worked on with a paper mill customer last quarter. They had a press roll shaft, which had a radial load of 12,000 lbs, running at 180 RPM, with an operating temperature of 160°F, using ISO 68 oil (which has a viscosity of 46 cSt at 160°F, per ISO standards). The bearing diameter was 6 inches, so we chose an L/D ratio of 1, making the bearing length 6 inches. The formula for radial load capacity of a hydrodynamic sleeve bearing is:
W = (P * D * L) / 1000
Where W is the load in thousands of pounds, P is the lubricant’s unit load capacity, measured in psi. To get P, we use a modified Raimondi and Boyd formula, the standard in the industry for hydrodynamic bearing performance. For this case, with L/D =1, viscosity of 46 cSt, and speed of 180 RPM, P works out to roughly 220 psi. Plugging in the numbers: W = (220 66)/1000 = 7.92 thousand lbs, or 7,920 lbs. Wait, that’s less than the customer’s 12,000 lb load. So what do we adjust? We can either increase the L/D ratio to 1.5 (making length 9 inches) or switch to a higher-viscosity oil, like ISO 100, which has a viscosity of 62 cSt at 160°F. Let’s recalculate with ISO 100 oil: P jumps to 280 psi, so W = (28066)/1000 = 10,080 lbs, still not enough. Increase L/D to 1.5, length 9 inches: W = (220 69)/1000 = 11,880 lbs, almost exactly the customer’s load. Perfect. That’s why adjusting geometry or lubricant viscosity is the first go-to fix for insufficient capacity. We also factored in the customer’s alignment tolerance—their shaft was slightly misaligned, so we added a 10% safety factor, bringing the recommended load to 13,000 lbs, which works out perfectly. That safety factor is non-negotiable, by the way. Operating at 100% of calculated capacity is a recipe for failure; we always recommend 15-20% extra capacity to account for unexpected overloads, temperature spikes, or slight misalignment that will pop up in real-world operation.
But here’s the thing: formulas are great, but they don’t account for every variable. That’s why we also use finite element analysis (FEA) for critical applications, like our custom bearings for gas turbines or marine engines. FEA lets us model how the bearing will deform under load, how the lubricant pressure distributes across the bearing surface, and how temperature changes will affect the film. For a customer building a new 5MW gas turbine, we used FEA to test three different bearing designs, each with a slightly different L/D ratio and lubricant grade, and found that a 7-inch diameter, 8-inch length bearing with ISO 150 oil would handle the full 25,000 lb radial load with a safety factor of 2, while also running 10°F cooler than the initial design they’d drawn up. That’s the kind of detail you can’t get from a basic formula.
Common mistakes beyond the ones I’ve already mentioned: forgetting about contamination. Fluid film bearings can’t handle dirt or metal particles in the lubricant—those particles act like sandpaper, scratching the bearing surface and breaking the film. When calculating load capacity, you have to adjust for contamination: if your oil has a cleanliness grade of ISO 18/15 (which is pretty dirty), you’ll need to increase your viscosity or bearing size by 15% to compensate, because particles will wear the film over time. We had a mining customer last year who skipped this step; their load calculation was perfect, but their oil system had a broken filter, and after 6 months, the bearing’s capacity dropped by 20%, leading to a catastrophic failure. Now, we always include oil cleanliness testing as part of our consultation, because it’s a free fix that makes a huge difference.
Another mistake: not accounting for dynamic loads. A lot of applications have loads that vary, like a rock crusher that’s sometimes hitting extra large rocks, or a pump that runs at 120% load during startup. Static load is easy to calculate, but dynamic load—loads that change over time, or peak during startup/shutdown—requires a different approach. For startup, when the lubricant is cold and thick, the film isn’t fully formed, so the metal parts touch, and load capacity is much lower. We recommend checking startup load separately and adjusting the bearing’s material to handle that, like using a babbitt lining, which is soft enough to wear slightly during startup without damaging the shaft, while still maintaining full load capacity when the bearing is up to operating temperature.

As a fluid film bearing supplier, my job isn’t just to sell you a bearing that fits your shaft. It’s to give you a bearing that will run for years without failing, so you don’t have to deal with unplanned downtime. The load calculation isn’t a black box—it’s a mix of science, experience, and understanding your specific application. If you’re a design engineer working on a new piece of equipment, or a maintenance manager troubleshooting a failing bearing, don’t rely on generic formulas or outdated spreadsheets. Reach out to our team to discuss your load requirements, lubricant specs, speed, and operating environment. We’ll walk through every step, adjust for all the variables, and make sure you get a bearing that not only meets your load-carrying needs, but is built to last in your unique operating conditions. We work with clients across industries, from pulp and paper to marine to renewable energy, so whatever your application, we have the expertise to help you calculate the right load capacity and find the perfect bearing for your needs.
Fluid Film Bearings If you have questions about load-carrying capacity, or need a custom bearing for your equipment, get in touch with our team today to discuss your requirements.
- Cameron, A. (1981). Principles of Lubrication. John Wiley & Sons.
- Raimondi, A. A., & Boyd, J. (1958). A Solution for the Finite Journal Bearing and Its Application to Analysis and Design, Parts I, II, and III. Transactions of the ASLE.
- Stachowiak, G. W., & Batchelor, A. W. (2014). Engineering Tribology (4th ed.). Elsevier.
- Bloch, H. P. (2006). Fluid Film Bearings: Selection and Application. McGraw-Hill.
- ISO 4386-1:2009, Plain bearings—Metallic plain bearing materials—Part 1: Babbitts.
Wenzhou Zhengbang Bearing Co., Ltd.
We are one of the most professional fluid film bearings manufacturers and suppliers in China. With abundant experience, we warmly welcome you to buy customized fluid film bearings at competitive price from our factory. If you have any enquiry about free sample, please feel free to email us.
Address: Units 1-1 and 3-1, Building 12, Yongxing Nanyuan Small and Micro Enterprise Startup Park, Binhai 2nd Road, Yongxing Subdistrict, Longwan District, Wenzhou City, Zhejiang Province.
E-mail: zbbearing@zbbearing.com
WebSite: https://www.zb-bearings.com/
